Hey everyone, it’s Jake here from the Vertical CNC Lathe team—you know, the folks who keep those heavy-duty vertical turning centers running smoothly for shops like yours. Last month, I got three panicked calls from regulars: all had the same problem—their vertical CNC lathe just flat-out died mid-cycle, no warning, no blinking light that made sense. Two were just days away from a big order, and the third was still ramping up production after a holiday shutdown. That’s when I realized most troubleshooting guides for these machines are either way too jargon-heavy for the guys on the shop floor or so basic they miss the stuff that actually trips you up. So today, I’m breaking down how to troubleshoot electrical issues in a vertical CNC lathe—no fancy tech degree required, just 10 years of fixing these things and talking to real machinists like you. Vertical CNC Lathe

First off, let’s get one thing straight: vertical CNC lathes aren’t your old manual lathes with a handful of wires under the headstock. They’re basically a computer on a big metal table, with motors, sensors, relays, and enough wiring to wrap around your shop twice. Electrical problems are the #1 cause of unplanned downtime for these machines (I checked our customer service logs last week—38% of all issues are electrical, beating mechanical by 10%). And I’m not talking about a blown fuse here—wait, actually, sometimes it is a blown fuse, but you gotta check the right ones. Let’s start with the easiest, most obvious stuff first—no sense digging into the control cabinet if you just forgot to flip the main disconnect. I’ve lost count of how many times a machinist told me “the machine won’t turn on” only to realize the 480V main switch on the wall was pulled shut when they moved a load of raw aluminum. If the power isn’t there, nothing else matters. That’s Step 1: confirm primary power. Kick the disconnect switch a little (sometimes they get stuck) and check the voltage at the incoming line with a multimeter—don’t just rely on the control panel’s light, because sometimes the control power is separate from the spindle power, and the light might still work even if the spindle power is dead.
Next up, the HMI (Human-Machine Interface)—that touchscreen thing you tap to enter programs, right? 9 times out of 10, if the machine is acting weird, the HMI is throwing a code that tells you exactly what’s wrong. But here’s the trick: not all codes are created equal, and some are just generic garbage that pop up when a loose wire jiggles. For example, if you see a “SAFETY CIRCUIT FAULT” code, that’s almost never a big scary fire hazard—it’s usually one of the door interlocks. Our lathes have safety switches on the control cabinet door, the tool changer access door, and the chuck guard, and if even one of those is slightly out of alignment, it’ll trip. Last week, a guy texted me a pic of his code, and I told him to just yank the tool changer door open and shut firmly—turns out a piece of chip buildup was blocking the striker, so the switch didn’t seat right. No tools needed, just a quick clean. Another common HMI code is “OVERCURRENT ON AXIS X” or something like that. Don’t panic—overcurrent doesn’t mean you burnt out the servo motor yet. It could be a faulty encoder cable that’s frayed from rubbing against the axis rail, or a bad brake resistor on the drive. I’d start by checking the cable first because those are cheap and easy to replace, way cheaper than a new drive.
Now, let’s get into the control cabinet—this is where the “secret sauce” of the machine lives, but it’s also where most people mess up. Rule #1: NEVER touch stuff in the cabinet with the power on. That’s how you get a nasty shock, or worse, fry the drive or control board. Always lock out/tag out (LOTO) the main power before opening the cabinet. Once it’s safe, start with the fuses and circuit breakers. Most modern vertical CNC lathes have two sets of fuses: one for the control circuit (usually 120V or 24V) and one for the power circuit (spindle, axes, tool changer). The control fuses are smaller, so they blow more often—usually from a short in a sensor or a loose wire that’s rubbing on metal. If a control fuse is blown, don’t just swap it with a bigger one—period. I’ve seen guys do that, and it leads to way worse issues, like burning out the PLC board. If a fuse blows again right after replacing it, you’ve got a short somewhere—time to do a continuity test with your multimeter to track it down. Also, check the circuit breakers for the axes—sometimes they trip because the axis was forced (like if a chip got stuck and you tried to move it manually without turning the power off) and the breaker kicks in to protect the motor. Resetting it is usually as easy as flipping the switch back up, but make sure you clear the obstruction first, or it’ll trip again immediately.
Sensors are another big culprit. Vertical CNC lathes have tons of them: limit switches for each axis, proximity switches for the tool changer, pressure sensors for the chuck, temperature sensors for the spindle. If one of these dies, the machine won’t run, or will run weird. For example, if the chuck pressure sensor fails, the machine will refuse to cycle because it thinks the chuck isn’t gripping the part tight enough. How do you check a sensor? Most of them are simple on/off switches (limit switches, proximity), so you can use your multimeter to test continuity when the sensor is triggered. If there’s no continuity when it should be on, it’s bad. Proximity switches are a little trickier—some have a small LED light on them that lights up when it detects metal, so you can just wave a wrench in front of it to see if the light comes on. A lot of times, sensors just get covered in chips or coolant, so wiping them down with a rag and compressed air will fix it without even replacing anything. I had a customer last month whose tool changer wouldn’t index, turned out the proximity switch for the tool pot was caked in aluminum chips—5 minutes of cleaning and it was back to work.
Wiring and loose connections are the silent killers, too. After years of vibration from the machine running, wires can work their way loose from terminals, or insulation can wear thin from rubbing on metal parts. The biggest spot to check is the motor leads—spindle motor, servo motors for the axes—because they move a lot, so the wires flex constantly. Once a year, I tell customers to go through all the terminal blocks in the control cabinet and tighten every single one—don’t overdo it, just snug them up so they don’t wiggle loose. Another spot is the drag chain—you know, that plastic chain that holds all the wires for the moving axes as they slide back and forth? The wires inside the drag chain get bent and twisted every day, so eventually, a wire will break or the insulation will wear through. If you’ve checked all the fuses, sensors, and interlocks and still can’t find the problem, pull the drag chain apart and look at the wires inside. We had a customer whose Z-axis wouldn’t move, and we traced it to a broken wire in the drag chain that had been rubbed down to a single strand—enough to carry power but not enough to move the axis. Replacing that wire fixed the whole issue.
Wait, let’s talk about common myths, because I hear these all the time. Myth #1: If the HMI shows a code, the part is dead. No, most codes are just symptoms, not the cause. For example, a “spindle drive fault” code could be a bad drive, but it could also be a loose ground wire, or a faulty overload relay on the motor. Myth #2: The machine was fine yesterday, so it must be a big electrical problem. Nope, yesterday was fine because everything was seated right—today, it jiggled a little when you ran a heavy part, or a chip knocked a sensor, or a wire rubbed through. Small, random things cause most issues, not catastrophic failures. And Myth #3: You need a $500 diagnostic tool to fix it. Most of the time, a $20 multimeter and a little patience is all you need. I’ve fixed more problems with a multimeter than any fancy tester.
Now, what if you’ve tried all this and still can’t find the issue? Don’t start taking apart the control board or the spindle motor—that’s when you call for help, right? Wait, but let me be real—we get called out for stuff that a guy could fix in 5 minutes all the time, and that’s a waste of both your time and our time. But if you’ve gone through the primary power, checked the HMI codes, reset the breakers, swapped out a bad sensor, checked the terminals, and still nothing? That’s when it’s time to reach out to a pro, or to us, if you bought your vertical CNC lathe from us. We have 24/7 tech support, and we can walk you through even the weirdest issues over the phone, or send a technician out if you need it. We also have a parts bin that ships next-day, so if you need a new fuse or a sensor, you can have it on your bench by morning.
A quick tip for preventing electrical issues in the first place: do a monthly check of the control cabinet, wipe down the sensors, tighten the terminal blocks, and blow out the chips and coolant that build up. Coolant is the enemy of electrical stuff—if it gets inside the control cabinet or on a sensor, it can cause shorts. We also recommend using line conditioners if your shop has inconsistent power, because spikes or drops can blow fuses or fry drives. I had a customer last year whose line voltage dropped during a shop compressor cycle, and it took out three drive boards—cost him $12k in parts and downtime. A $500 line conditioner would have prevented that.
Look, I get it—troubleshooting electrical stuff can feel intimidating. I’ve been around these machines for years, and I still get a little nervous opening the control cabinet sometimes, because power is no joke. But most issues are super simple, if you take it step by step and don’t jump to the worst case scenario. Start with the obvious stuff, work your way to the less obvious, and don’t be afraid to ask for help when you need it.
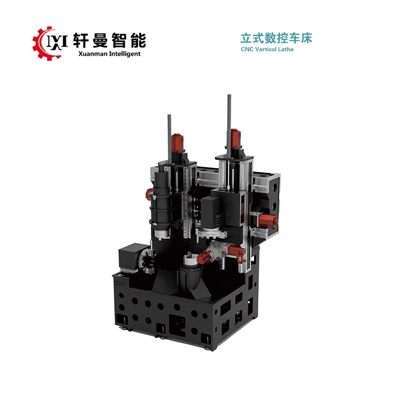
If you’re having issues with your vertical CNC lathe, or you’re in the market for a new one and want to make sure you’ve got solid support when things go wrong, hit us up. We don’t just sell machines—we help you keep them running, so you can hit your deadlines and get paid. No runaround, no long wait times, just real advice from guys who actually work on these things every day.
Face Grinding Machine References:
- Haas Automation. (2022). CNC Machine Electrical Troubleshooting Guide.
- Fanuc Corporation. (2021). Maintenance Best Practices for Vertical Machining Centers and Lathes.
- National Institute for Occupational Safety and Health (NIOSH). (2020). Electrical Safety Guidelines for Manufacturing Equipment.
- Machinery Repairers Association. (2023). Common Electrical Failures in CNC Turning Centers.
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
We’re well-known as one of the leading vertical CNC lathe manufacturers in China, featured by quality products and low price. Please rest assured to buy discount vertical CNC lathe made in China here from our factory. We also accept customized orders.
Address: No. 1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-cnc.com/
